
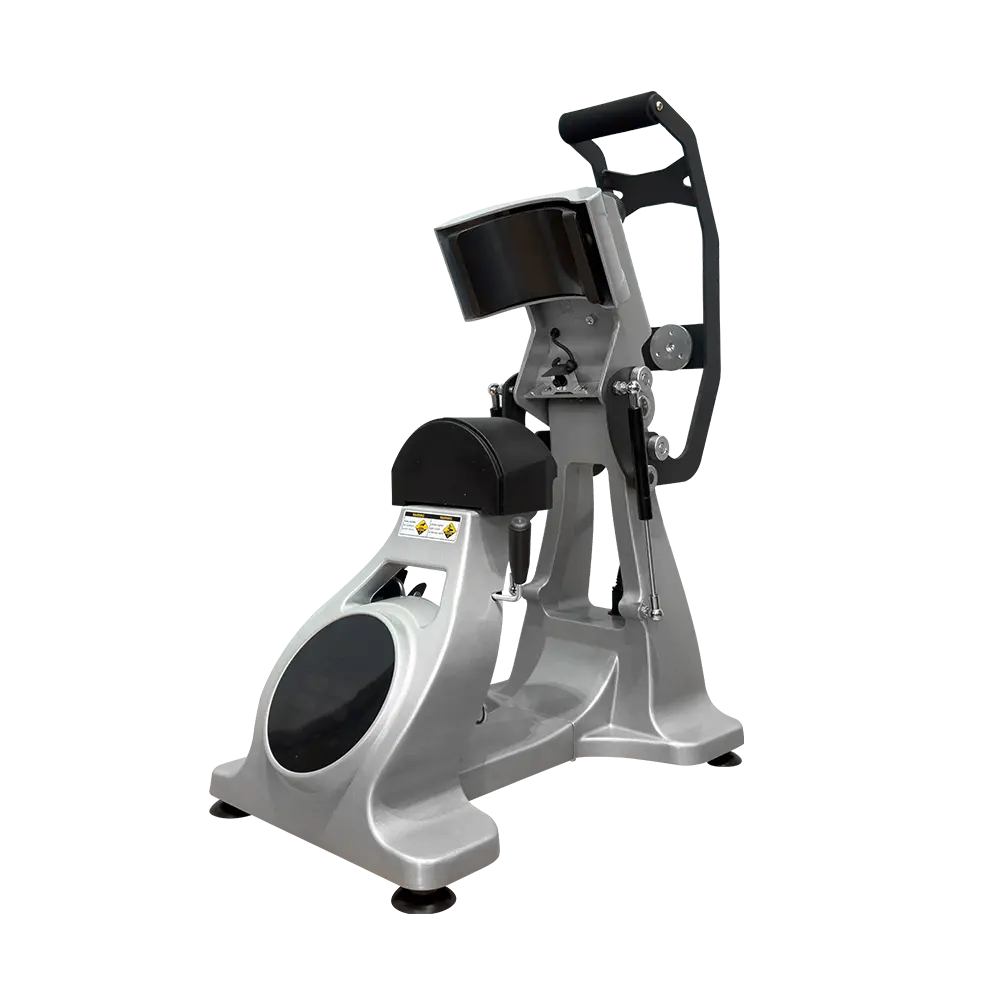
Decorating dimensional headwear presents physical challenges distinct from standard flat garment decoration. Curved surfaces, center seams, reinforced buckram, and rigid visors create irregular contact planes. Achieving clean, repeatable transfers on structured six-panel caps or delicate performance fabrics requires machinery built with rigid tolerance controls and dedicated heating profiles. Investing in a professional kappenpresse provides high-volume contract decorators and apparel manufacturers with the structural rigidity and thermal consistency needed to handle complex geometries without scorch marks, graphic distortion, or substrate deformation.

Flat heat platens operate on simple planar contact, but headwear pressing demands continuous, uniform surface contact across a radial arc. Standard caps range from low-profile, unstructured five-panel designs to steep, high-profile structured six-panel trucker hats. When the curvature of the upper heating platen does not match the curvature of the lower base platen, pressure concentrates strictly along the highest arc line, leaving the periphery under-pressed.
To eliminate migration and poor adhesive bonding, professional equipment employs cast aluminum heating elements machined with exact radial tolerances. The thermal transfer process relies on direct conductive heat transmission. If air gaps exist between the transfer carrier and the cap crown, heat transfer drops exponentially. A precision-engineered kappenpresse integrates matched upper and lower radii, ensuring that every millimeter of the transfer receives equal thermal exposure and mechanical force throughout the press cycle.
Uniform heat distribution across the arc of an upper platen depends entirely on the design of the internal resistance elements. Lower-tier machines often use sparse tubular heating elements, creating localized hot spots along the central spine and cold zones near the perimeter. Industrial-grade manufacturing addresses this issue by embedding continuous, serpentine heating coils directly into high-density aluminum alloy platens.
Embedded Cast Elements: Provide high thermal mass and resistance to ambient temperature drop during high-cycle loading sequences.
Surface Milled Profiles: Allow for microscopic surface flatness across the curved plane, reducing cold boundary layers.
Dual-Probe Monitoring: Ensures real-time PID feedback directly from the operational contact face rather than secondary junction points.
Thermal stability prevents common transfer failures, such as adhesive under-curing at the seam margins or dye sublimation color shift caused by localized overheating. Industrial units designed by Heat Press Leader feature balanced heat loops that maintain a variance of less than 1.5% across the entire operational pressing field.
Achieving sufficient clamping force on a curved platen demands robust structural mechanics. Manual over-center linkages and pneumatic cylinders must translate linear force into distributed radial pressure. When mechanical frames flex under load, the clamping angle changes, causing downward force to push the substrate forward rather than compressing it perpendicularly against the lower base.
Heavy-gauge laser-cut steel frames eliminate structural deflection. By retaining frame rigidity under continuous forces exceeding 4 bar (pneumatic) or high-leverage manual lock-down, the platen maintains parallel contact along the entire arc. This rigid alignment prevents the cap from shifting, protecting fine-line screen printed transfers, direct-to-film (DTF) films, and embroidered patches from registration blur or thermal ghosting.
One of the primary difficulties in cap decoration is keeping the fabric taut against the lower platen without manual operator intervention during closure. Unsecured fabric bunches at the base, creating wrinkles along the lower crown and near the sweatband.
Independent Rear Clamping: Secures the rear sweatband and excess fabric downward, pulling the front panel flat against the curvature.
Adjustable Tension Arms: Accommodate variable material thicknesses, from thin polyester performance blends to heavy brushed cotton and wool blends.
Quick-Release Lower Bases: Allow operators to swap platen profiles in seconds, matching youth, standard, or oversized headwear formats without secondary tooling.
Six-panel caps present a prominent center seam constructed with thick polyester thread and internal reinforcement tape. When pressing standard DTF or plastisol transfers over this seam, the raised thread profile absorbs the bulk of the downward force, preventing the transfer from seating into the surrounding fabric valley. Specialized silicone pads and milled seam trenches within the lower platen allow the raised seam to sink below the baseline surface, equalizing downward force across the entire graphic area.
Structured caps utilize a stiffened inner buckram backing behind the front panels. Excessive dwell time or uncontrolled heat softens this buckram, causing the cap structure to collapse or leave permanent shiny marks on synthetic twill. Modern production facilities select a heavy-duty kappenpresse equipped with micro-step digital controllers to program short, high-pressure cycles that bond adhesive layers without compromising internal buckram polymers.
Operational workflow in commercial print facilities requires continuous cycling without thermal recovery lag. Standard manual swing-away or clamshell units can bottleneck high-capacity screen print and embroidery workflows. Industrial installations prioritize pneumatic operation and multi-station rotary or shuttle platforms to drive continuous production.
Pneumatic drive systems deliver repeatable, digitally regulated pressure settings independent of operator fatigue. Facilities can lock in exact parameters (temperature, time, and PSI) across multiple shifts, ensuring standard output on sensitive materials such as water-repellent nylon, acrylic knit, and recycled PET fabrics.
| Platform Type | Primary Application | Throughput Velocity | Pressure Consistency |
|---|---|---|---|
| Manual Clamshell | Short runs, sampling, low-profile unlined caps | Moderate (Operator dependent) | Variable (Manual leverage) |
| Pneumatic Single-Station | Medium-to-large runs, heavy patches, dense twill | High (Auto-release cycles) | Absolute (Regulated air line) |
| Dual-Station Shuttle / Rotary | Continuous contract fulfillment, mixed sku production | Maximum (Concurrent prep and press) | Absolute (Independent platen control) |
Integration of modular fixtures manufactured by Heat Press Leader allows facilities to switch effortlessly between cap crown decoration, bill decoration, and sleeve transfers using a single industrial base frame.
High-volume thermal application requires structured verification procedures to ensure graphic wash-fastness and adhesion integrity. Surface temperature should be validated using calibrated non-contact infrared sensors or surface contact thermocouples across nine test points along the platen arc.
Adhesion peel tests must be conducted after the substrate has completely cooled to ambient temperature. Evaluating the adhesive flow beneath high-magnification lenses reveals whether the hot-melt polyurethane layer has properly encapsulated the fabric fibers or merely formed a superficial surface bond. Industrial machinery must hold target temperatures within tight margins to achieve this full fiber encapsulation without scorching delicate outer yarns.
Q1: Why do structured six-panel caps often show ghosting or weak
adhesion along the center seam?
A1: The raised ridge of the center
seam absorbs most of the platen force, creating microscopic air pockets on
either side of the thread. Using lower platens with central seam grooves or
applying specialized high-density silicone pads distributes the load evenly over
the seam profile.
Q2: How does pneumatic actuation improve consistency compared to
manual press mechanisms?
A2: Pneumatic systems use continuous air
pressure through calibrated pneumatic pistons, applying an identical, measured
force on every cycle regardless of operator physical strength. This consistency
eliminates variation in adhesive flow and prevents substrate burning caused by
over-clamping.
Q3: What causes synthetic cap fabrics to develop a shiny or scorched
appearance during heat pressing?
A3: Scorch marks and shine occur
when high heat melts or crushes outer thermoplastic fibers (polyester, nylon).
Using accurate digital heat controls, reducing dwell times, utilizing teflon
platen covers, and selecting lower-melt adhesive transfers prevents thermal
damage to sensitive fibers.
Q4: Can a single curved base platen handle both low-profile and
high-profile trucker hats effectively?
A4: While minor adjustments
can be made using hold-down tension, low-profile and high-profile caps possess
fundamentally different crown angles. Industrial production environments utilize
modular, quick-change lower base platens shaped specifically for shallow or
steep crown angles to maintain parallel clamping force.
Q5: What is the recommended method for verifying the platen
temperature on a curved press?
A5: Contact surface thermocouples or
calibrated thermal test strips placed across the curved face offer the most
accurate readings. Non-contact infrared pyrometers can yield inaccurate data due
to emissivity variations on bare or coated aluminum platens.
Scaling commercial cap decoration requires equipment built to exact mechanical parameters, matching specific production volumes, fabric blends, and transfer technologies. Engineering teams and facility managers seeking customized platen geometry, automated pneumatic systems, or high-volume dual-station configurations can submit production specifications directly. Contact our engineering department to discuss custom tooling dimensions, pneumatic integration requirements, and multi-station press development tailored to your industrial workflow.


