
Decorating dimensional headwear presents physical challenges unlike those encountered in standard flat-garment production. Flat textiles allow uniform downward clamping pressure across an unobstructed plane. Caps, by contrast, are three-dimensional structures constructed from multiple curved panels, reinforced with stiff buckram backings, and interrupted by raised, multi-layered seams. Applying heat transfers, plastisol prints, embroidered emblems, or Direct-to-Film (DTF) films to these curved surfaces demands dedicated thermo-mechanical systems designed specifically for compound radii.
Achieving durable adhesion without scorched fabric, shiny polyester marks, or blurred transfers requires balancing platen geometry, thermal conductivity, clamping mechanism kinematics, and textile tension control. Production facilities scaling their custom headwear output rely on specialized machinery where lower platen geometry and upper heating elements mirror the natural curve of the crown.

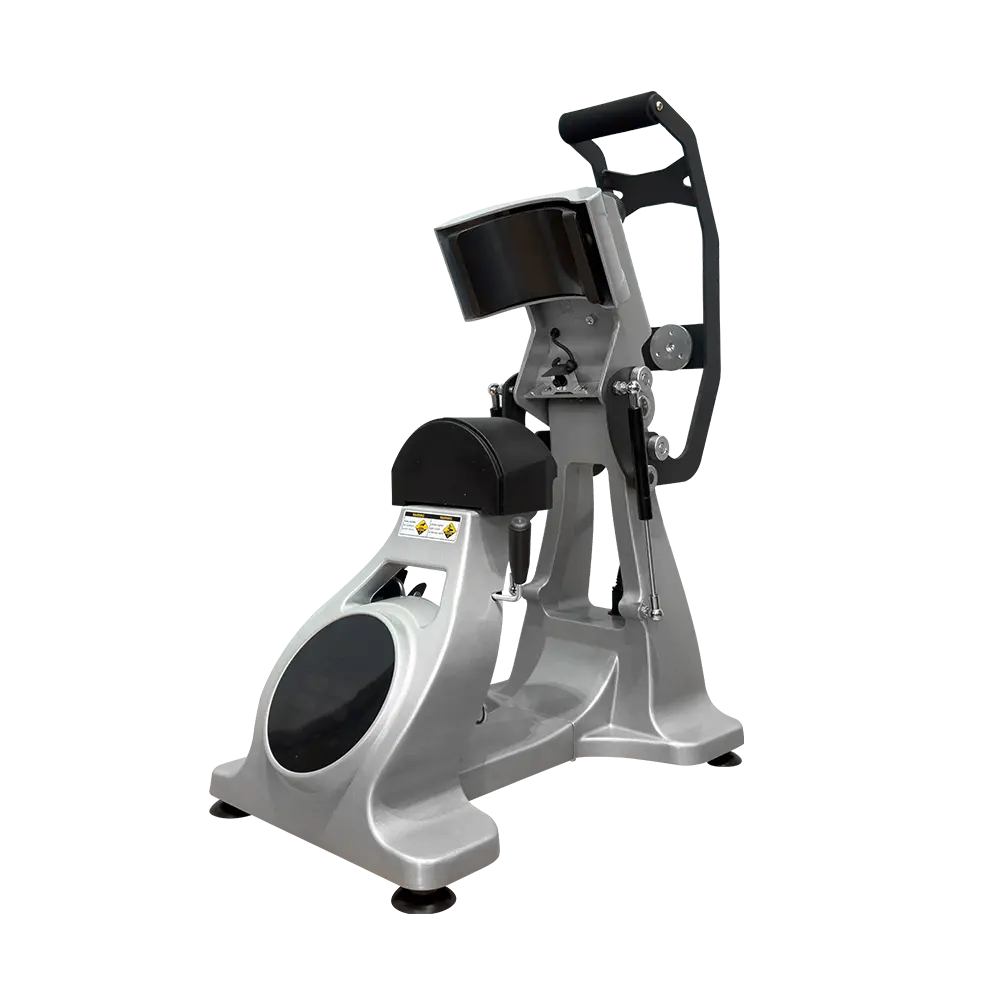
The primary engineering objective during headwear thermal application is distributing load evenly over a compound arc. Standard flat heat presses exert vertical, single-axis force. If applied to a cap, this linear force concentrates on the highest peak of the crown, crushing the structure while leaving the perimeter without sufficient contact pressure. A purpose-built heat press cap mechanism resolves this through matching radial upper and lower platens that form a continuous pressure zone along both the vertical and horizontal axes of the front panels.
Industrial machinery accomplishes this uniform engagement through specific mechanical systems:
Concentric Platen Curvature: The upper heated cast-aluminum element and the lower silicone-padded base platen share an aligned radius of curvature. This prevents edge-pinching at the top of the crown and pressure drop-offs near the sweatband.
Progressive Cam-Action Clamping: Rather than closing flat, the hinge geometry rolls down smoothly onto the curved surface, expelling trapped air pockets between the transfer film and the cap fabric.
Dual-Pivot Pressure Adjustment: Advanced units feature micro-adjustable center-point pressure screws that ensure the down-force vectors remain perpendicular to the tangent of the platen curve at every point of contact.
Thermal management within these curved platens requires careful calibration. Cast-in tubular heating elements must be coiled with tighter density near the outer perimeter of the upper casting to counter convective heat loss along open edges. When high-volume manufacturing lines partner with Heat Press Leader, platen assemblies incorporate embedded PID temperature controllers and precision resistance temperature detectors to maintain thermal variance within a tight +/- 2°F tolerance across the entire curved surface.
Headwear styles differ vastly in construction, fabric density, and reinforcement layers. Each profile reacts uniquely to high temperature and clamping loads.
Structured hats, such as classic 6-panel baseball caps and high-crown trucker caps, feature a stiff buckram backing laminated to the interior of the front panels. This woven or non-woven layer provides shape retention. Excessive heat or prolonged dwell times can soften the buckram adhesive, causing it to bleed through face fabrics or shrink, creating permanent surface puckering. Unstructured dad hats lack this internal reinforcement, requiring higher surface tension from lower hold-down clamps to prevent the fabric from gathering and creasing under pressure.
In standard 6-panel caps, a thick vertical seam bisects the front decoration area. This structural junction comprises multiple fabric layers, inner bias tape, and heavy stitching thread. Under a rigid press platen, this raised ridge bears the entirety of the clamping load, creating a "bridge" that lifts the heated platen 0.5mm to 1.5mm away from the adjacent fabric. Transfers applied across this seam frequently fail along the immediate valley on either side. Overcoming this requires high-rebound silicone base pads (typically 30 to 50 Durometer Shore A) that deform around the raised seam, maintaining continuous contact across the low points.
Modern headwear integrates a broad array of fibers, each demanding tailored press settings:
100% Heavyweight Cotton Twill: High thermal tolerance (320°F–350°F), low risk of surface glazing, but requires sustained dwell times to ensure heat penetrates deep twill grooves.
Polyester and Poly-Spandex Blends: Prone to dye migration where dispersed dyes sublimate into the transfer adhesive at temperatures above 285°F. These require low-temperature, fast-reacting adhesive systems and platens with rapid heat recovery.
Recycled PET Performance Fabrics: Highly sensitive to heat marking and mechanical crush; requires lower surface pressures paired with exact dwell timing to preserve moisture-wicking and water-repellent coatings.
Substrate stability during the pressing cycle determines transfer registration accuracy. When operating a commercial heat press cap, the operator must secure the cap tightly over the lower form to eliminate slack and prevent movement during platen engagement.
Industrial machines utilize dynamic hold-down mechanisms. A rear-mounted mechanical clamp captures the cap’s sweatband and inner rear hem, pulling the crown downward and backward over the lower platen. This mechanical stretch smooths out wrinkles, locks the center seam flat against the silicone pad, and leaves both hands free for precise graphic positioning.
Production environments handle varying crown heights, from low-profile running visors to deep-crown snapbacks. Fixed-size platens limit versatility. Modular machines feature quick-release lower platens in targeted sizes:
Standard Crown (4" x 8"): The universal baseline for standard 6-panel and 5-panel structured athletic headwear.
Low-Profile / Youth (2.75" x 6.5"): Engineered for fitted dad hats, unstructured caps, and children’s sizes where standard forms would over-stretch the fabric.
High-Crown / Trucker (4.5" x 8.5"): Matches the steep front angle of modern foam-front and structured snapback headwear.
Visor / Bill Specialty Forms: Narrow, elongated fixtures designed for transfers placed directly along curved brims or side-panel runs.
Apparel decorators employ diverse decoration methods on headwear. Each technology requires a specific combination of temperature, pressure, dwell time, and peel technique.
DTF has become a dominant method for headwear due to its elasticity and fine detail resolution. Polyurethane hot-melt adhesive powders typically activate between 265°F and 300°F. The challenge on curved surfaces lies in preventing the PET carrier film from shifting during upper platen release. Auto-open mechanisms with magnetic dampening or controlled pneumatic exhaust prevent sudden upward jolts that cause carrier film separation before the adhesive cools.
Sublimation involves transforming dye particles into gas at temperatures near 380°F to 400°F. This process requires absolute contact uniformity. Any gap between the transfer paper and the polyester fabric allows dye gas to disperse laterally, causing fuzzy edges or ghosting. Sublimation on caps requires firm, uniform pressure and heat-resistant thermal tape to anchor the graphic securely to the crown.
Dimensional patches present significant thickness variations. Heat-activated backings (such as polyamide or EVA adhesives) must be liquefied without scorching the raised embroidery threads or decorative faux leather face. Top-down heating alone often takes too long to penetrate thick emblems, potentially marking the outer fabric. High-performance machinery developed by Heat Press Leader addresses this challenge with bottom-heated lower platen configurations, driving thermal energy upward through the cap crown directly into the patch adhesive layer.
Process deviations during production runs lead to scrap rates and reduced output. Identifying mechanical and operational causes helps streamline line adjustments:
Perimeter Transfer Lifting: Often caused by an upper platen radius that is too flat relative to the lower platen, creating adequate pressure in the center while leaving edges unsealed. Adjust lower platen silicone thickness or swap to a narrower profile form.
Fabric Glazing / Surface Sheen: Occurs when excessive heat and localized pressure flatten synthetic fibers. Lower the operating temperature, reduce the mechanical down-force, and cover the upper platen with a PTFE non-stick wrap.
Wrinkling Along Lower Seams: Indicates insufficient hold-down tension. Ensure the cap's internal sweatband is fully flipped outward and locked securely by the hold-down stretcher before swinging the heater into position.
Ghosting / Image Doubling: Caused by the transfer paper shifting slightly while the adhesive is still molten. This typically happens when manual clam presses snap open aggressively. Dampened release systems stabilize the platen at cycle completion.
Facilities scaling from bespoke craft production to industrial batch runs must evaluate the mechanical drive systems of their equipment.
Manual toggle-clamp machines rely entirely on operator leverage. While portable and straightforward, output consistency over extended shifts can vary as operator fatigue affects clamping pressure repeatability. In contrast, pneumatic and electromagnetic systems automate the down-force stroke.
Pneumatic cap systems use compressed air cylinders to apply exact, repeatable pressure regardless of minor material thickness changes across different production runs. When integrated into high-speed decoration cells, an automated heat press cap station with dual shuttle tables allows an operator to unload and prepare a cap on one station while the alternate station executes a timed heating cycle under continuous mechanical hold.
A1: Flat platens make point contact only on the highest projection of the crown, crushing the buckram structure while failing to reach the lower curves and side panels. Dedicated curved platens apply continuous radial pressure perpendicular to the curved surface of the headwear.
A2: A raised center seam absorbs the majority of the downward platen force, creating a low-pressure gap along both sides of the seam. This gap prevents full adhesive melt. Using high-rebound, heat-resistant silicone lower pads helps absorb the seam height and maintain pressure across the entire surface.
A3: Silicone pad durometer defines the balance between firmness and flexibility. A medium-soft pad (around 30–40 Shore A) compresses around eyelets, panel seams, and crown stitching to ensure even pressure, while a harder pad (50+ Shore A) is better suited for flat, unstructured fabrics requiring sharp transfer definition.
A4: Tensioners pull the sweatband and rear panels backward, locking the front panel flat against the curvature of the base platen. This mechanical tension prevents fabric movement during pressing and stops the transfer carrier from lifting prematurely when the press opens.
A5: High-performance platens utilize serpentine or perimeter-wound cast-in heating elements that feature denser element spacing along the outer edges. This design counteracts natural convective edge cooling and maintains uniform temperatures from center to border.
Configuring commercial decoration lines requires machinery tailored to specific cap profiles, adhesive chemistries, and daily volume requirements. For custom platen geometries, OEM/ODM machinery integration, or pneumatic production lines, contact our engineering sales department to submit your production specifications and request an industrial equipment quotation.


